
 English
 русский
 Français
 Español
 Português
 Deutsch
 عربى

Lolita Pink Candy Crystal TPU Wrap Film is a celebration of sweetness, femininity, and playful luxury. Inspired by the delicate, candy-like aesthetics...
See Details
Home / News / Industry News / Surface Preparation Explained: Methods, Standards, and Film Prep Steps
Surface Preparation Explained: Methods, Standards, and Film Prep Steps
Content
- 1 What Surface Preparation Actually Means
- 2 Why Preparation Decides Whether the Job Survives
- 3 Mechanical, Chemical and Thermal Methods Compared
- 4 Preparation for Paint Protection Film, Window Film and Architectural Film
- 5 Standards, Tolerances and Verification
- 6 Where Preparation Goes Wrong
- 7 Frequently Asked Questions
Nine of ten adhesion failures on a film or coating line are decided in the twenty minutes before the product is even opened. Dust, silicone, hand oil and leftover adhesive from an old film all sit between the substrate and the new layer, and no squeegee technique can compensate for what is underneath.
Surface preparation is the invisible half of installation work. A panel can look spotless under shop lighting and still fail a water break test, because the contamination that matters is measured in nanometres, not in fingerprints. This guide covers what preparation actually involves, how the mechanical, chemical and thermal families differ, and why the same principles apply whether you are blasting steel for an industrial coating or wiping a bonnet before paint protection film goes on.
What Surface Preparation Actually Means
Surface preparation is the combination of mechanical, chemical and physical treatments applied to a substrate before paint, coating, adhesive or protective film is applied, so that the bond forms at the interface instead of on top of a contamination layer.
Strip away the equipment names and every preparation process has to accomplish three things:
- Remove anything that does not belong on the substrate: oil, grease, dust, rust, mill scale, mould release agent, polish residue or old adhesive.
- Create the right bonding condition, which means an anchor profile for heavy coatings or a clean, high-energy surface for pressure-sensitive adhesives and films.
- Hold that condition until the product is applied, which comes down to temperature, humidity, airborne contamination and time.
Those three goals explain why one term covers sandblasting a storage tank and wiping down a bonnet with panel prep. The mechanism is completely different; the objective is identical.
Definition: a surface is prepared when it wets out evenly, carries no removable contamination, and can hold a bond under load, heat and moisture for the service life of the system.
Why Preparation Decides Whether the Job Survives
Adhesion is an interfacial property, which means the bond only forms where the adhesive, coating or film can physically wet the substrate, so anything sitting on that surface becomes the weakest layer in the whole system.
That is measurable, not philosophical. Silicone polish, hand oils and buffer residue drop the surface energy of automotive clear coat below the level at which a pressure-sensitive adhesive wets out completely. The film may still hold on installation day; the failure shows up later as edge lift, blistering after the first hot afternoon, or a patch that peels away with topcoat attached to it.
38-45mN/m surface energy of properly cleaned clear coat
Under 30mN/m reading typical of a silicone-contaminated panel
4 hourscommon maximum hold time for blasted steel
4B-5BASTM D3359 tape result expected from sound prep
Field rule: if the water break test shows water pulling back into beads within thirty seconds, the panel is not ready, no matter how clean it looks under a work light.
Mechanical, Chemical and Thermal Methods Compared
Mechanical, chemical and thermal preparation are not competing options; they are stages, and most working specifications combine at least two of them in a fixed order.
| Method | How it works | Typical applications | Main risks |
| Mechanical | Abrasive blasting, sanding, grinding and needle scaling cut or profile the surface. | Steel structures, weld seams, aged paint, aluminium castings. | Too coarse a profile traps air and causes pinholes or bridging. |
| Chemical | Solvent wiping, alkaline degreasing, acid etching and adhesion promoters lift or neutralise contamination. | Shop panels, glass, plastics, pretreated metal. | Solvent that flashes off before it lifts the oil simply moves residue around. |
| Thermal | Flame treatment, plasma and corona discharge raise surface energy by oxidising the top layer. | Polypropylene bumpers, plastic trim, other low-energy substrates. | Over-treatment embrittles the surface and creates a weak boundary layer. |
Sequence matters more than equipment. Solvent cleaning comes first to release oil, abrasion follows, and a second solvent wipe removes what the abrasive loosened. Skip that second wipe and you have ground contamination deeper into the profile. Compressed air deserves the same suspicion: without an oil and water separator, blow-off adds exactly the contamination you just removed.
Solvent before abrasion, solvent after abrasion. The first wipe removes the oil, the second removes what the abrasive lifted.
Preparation for Paint Protection Film, Window Film and Architectural Film
For paint protection film and window film the target is a smooth, fully decontaminated surface with no abrasion profile, which is the opposite of what blasted steel needs.
Wash, then decontaminate with iron fallout remover and tar remover, and clay the panel. Bonded particles telegraph through a clear film and cannot be pushed out later.
Polish or compound only if the paint needs correction, then strip the polishing oils with panel prep or a 30 percent isopropyl alcohol solution using a two-cloth method.
Blow out gaps, badges and edges with filtered air, then tack the surface. Edges are where lift starts, so they get the most attention.
Apply inside the working window, at roughly 18 to 28 degrees Celsius and 40 to 60 percent relative humidity, and keep silicone detail sprays away from the bay.
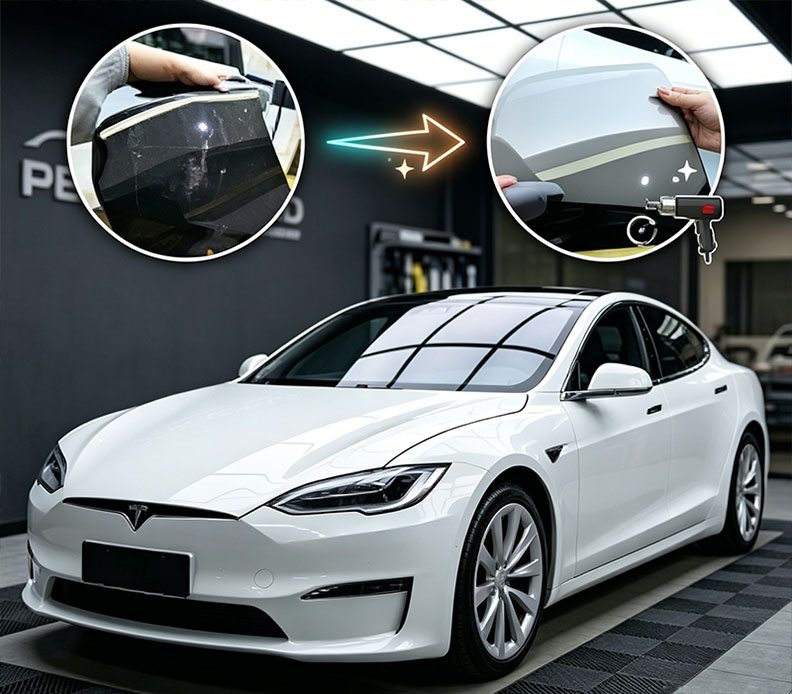 Instant Self-Healing TPU Clear Paint Protection FilmSelf-healing clear TPU PPF for automotive paint protection, with ambient-temperature swirl recovery, hydrophobic stain resistance, and customizable thickness for installers.View Product →
A self-healing topcoat can erase wash marks and light swirls, but it cannot rescue a panel that was wiped with a dirty rag. That is why a documented prep routine sits upstream of any film choice, and why shops working on high-end paint tend to standardise on one clear film system rather than switching products between jobs.
Glass is a different substrate with its own failure mode. Mineral water spots, soap residue and frame sealant all interfere with adhesion, so the pane is polished with a cerium oxide compound to lift deposits, cleaned with a film-safe solution and wiped dry before the film is cut and positioned.
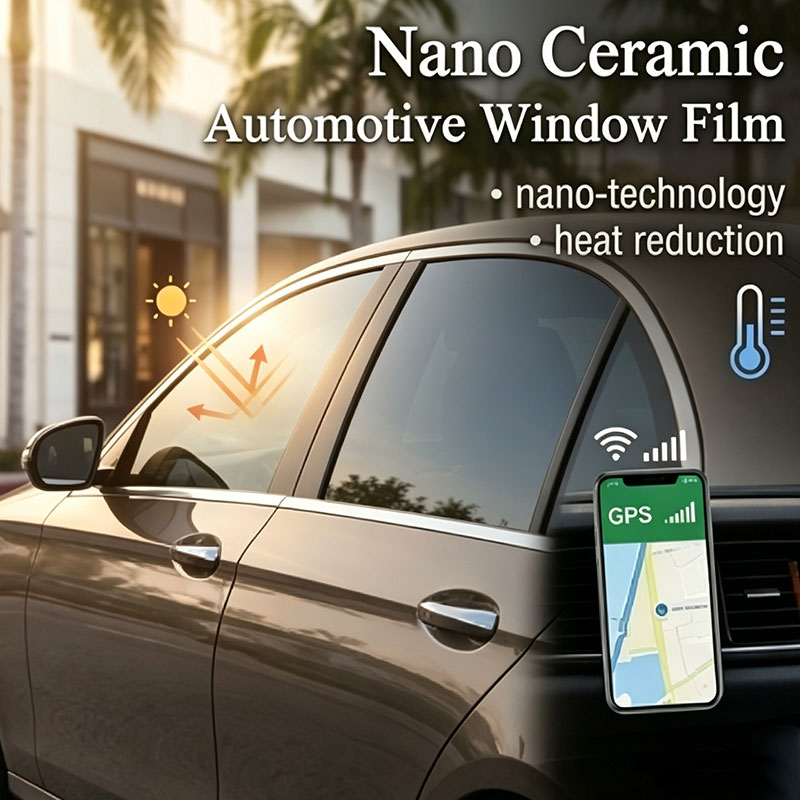 Nano Ceramic Automotive Window Film with Signal-Friendly ClarityFor automotive glass needing clear visibility and heat rejection, this nano-ceramic automotive film offers UV protection, IR rejection, and signal-friendly performance.View Product →
Architectural film raises the stakes because the panes are large, vertical and often inaccessible. Dust control, staged cleaning and a strict no-touch rule for cleaned glass matter far more than speed, since one speck can mean stripping an entire pane.
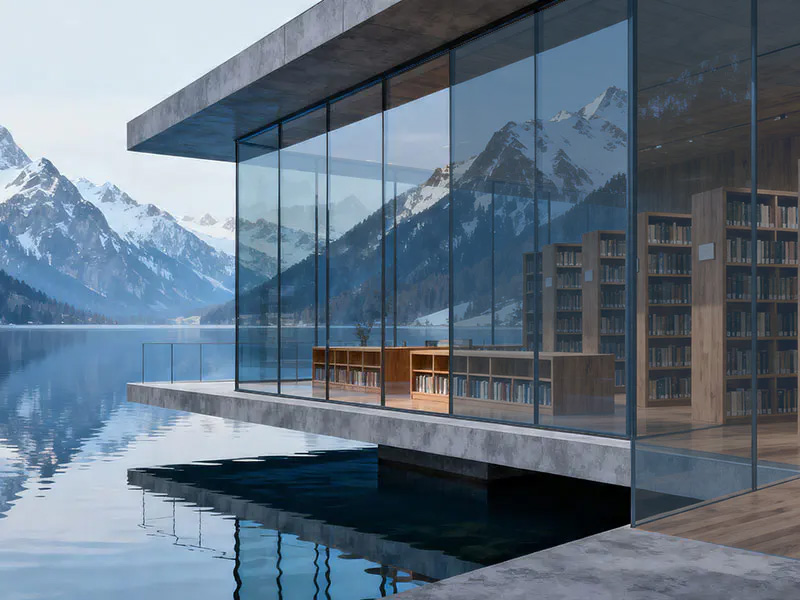 Architectural Window Film for Solar Control and SafetyFor large vertical glazing where installation discipline matters, this architectural film offers solar heat rejection, UV filtering, and safety versions in 2-mil or 4-mil.View Product →
Contamination control beats contamination removal. Covers, clean gloves and a fresh lint-free wipe cost a fraction of one re-do.
Standards, Tolerances and Verification
Verification is what separates a repeatable preparation process from a hopeful one, because every stage should carry a number, a test or a visible pass-fail result.
| Standard | Scope | Practical use |
| SSPC-SP1 | Solvent cleaning | Removes oil, grease and soil before any other step. |
| SSPC-SP10 / NACE No. 2 | Near-white blast cleaning | Steel in immersion or severe service environments. |
| ISO 8504 | Preparation methods | Framework for choosing mechanical, chemical or thermal routes. |
| ASTM D4285 | Oil and water in compressed air | Checks blast and blow-off air quality. |
| ASTM D4417 | Surface profile | Confirms anchor profile depth after blasting. |
| ASTM D3359 | Tape adhesion | Verifies the bond after application. |
Numbers on a spec sheet only help if somebody checks them. The water break test and contact angle readings are the fastest field checks, and both point the same way: the lower the angle, the better the surface wets out.
Water contact angle as a readiness check
Log the dew point, substrate temperature, cleaning products and hold time. A written prep record turns an argument about a failed panel into a five-minute answer.
Shops that run preparation as a controlled process, with the same discipline they apply to incoming and in-process quality control, usually see the difference in warranty claims rather than in day-one appearance.
Where Preparation Goes Wrong
Most preparation failures are process failures rather than product failures: the wrong sequence, a wipe that has already picked up oil, or a surface that was cleaned properly and then contaminated again before application.
Signals of a contaminated surface
Water beads and rolls off within seconds, film edges lift within 24 to 48 hours, blisters appear after the first heat cycle, and tape testing pulls film away with contamination visible on the adhesive.
Signals of a prepared surface
Water sheets out and holds a thin film for at least thirty seconds, a gloved hand slides without dragging, edges stay down after 72 hours, and tape testing returns 4B to 5B.
The same failures repeat across shops and substrates. Watch for these five:
- Wiping with a cloth that has already loaded up on oil, which spreads contamination instead of removing it.
- Cleaning the face of a panel but ignoring edges, gaps, badges and the shadow lines where film will be tucked.
- Using compressed air with no oil and water separator, undoing a clean surface in a single pass.
- Cleaning a panel hours or days before application, then leaving it open to dust, overspray and airborne grease.
- Stopping solvent work when the rag looks clean, rather than flipping to a fresh face and finishing with a dry wipe.
If a panel has to be re-cleaned after every attempt, the problem is usually the wipe, the cloth or the bottle, not the technique.
Understanding how a film or coating actually bonds at the molecular level makes the sequence easier to remember; this breakdown of thin film coating and deposition basics is a useful reference for teams that want the reasoning behind the checklist.
Frequently Asked Questions
What is surface preparation in simple terms?
It is every step taken to make a surface clean, chemically receptive and structurally ready before a coating, adhesive or film is applied. In practice that means cleaning, degreasing, abrading or activating, re-cleaning and verifying.
Do you need to sand a panel before applying paint protection film?
No. Abrasion exists to give coatings a mechanical anchor profile. Film bonds through a pressure-sensitive adhesive, so the goal is a smooth, fully decontaminated surface; sanding leaves scratches and a profile that traps air.
How do you know a surface is clean enough?
Use a water break test: distilled water should sheet out and hold a continuous film for at least thirty seconds. Tape tests to ASTM D3359 and contact angle readings confirm the result with numbers. If water beads immediately, clean again.
How long can a prepared surface sit before application?
As a working rule, apply film within an hour in a controlled bay and coat blasted steel within about four hours in normal conditions. Humidity, dust and airborne oil shorten both windows quickly, so preparation should be the last step before the product is opened.
The shortest useful prep checklist: degrease, abrade if the system needs it, re-clean, verify, then apply without delay.
Related products
-
-
Kemora Grey Satin Crystal TPU Car Film offers a distinguished, European-inspired gray tone with a refined satin crystal finish that sits elegantly bet...
See Details -
Dreamy Volcanic Ash is a dual-color chameleon TPU paint protection film offering a poetic, otherworldly color palette inspired by the soft grey-purple...
See Details -
Iridescent Blue Diamond White is a dual-color chameleon TPU paint protection film that combines the sparkling, multi-faceted brilliance of blue diamon...
See Details
GET THE LATEST QUOTATIONS
-
 No. 5, Datang Road, East District, Development Zone, Guangde City, Xuancheng City, Anhui Province,242200, China
-
 [email protected]
-
 +86 18170340295
PRODUCTS
MOBILE WEB
Copyright Anhui He He New Materials Co., Ltd. All Rights Reserved.
 Wholesale TPU PPF Film Automotive TPU PPF Manufacturer